Hot Products


0102030405
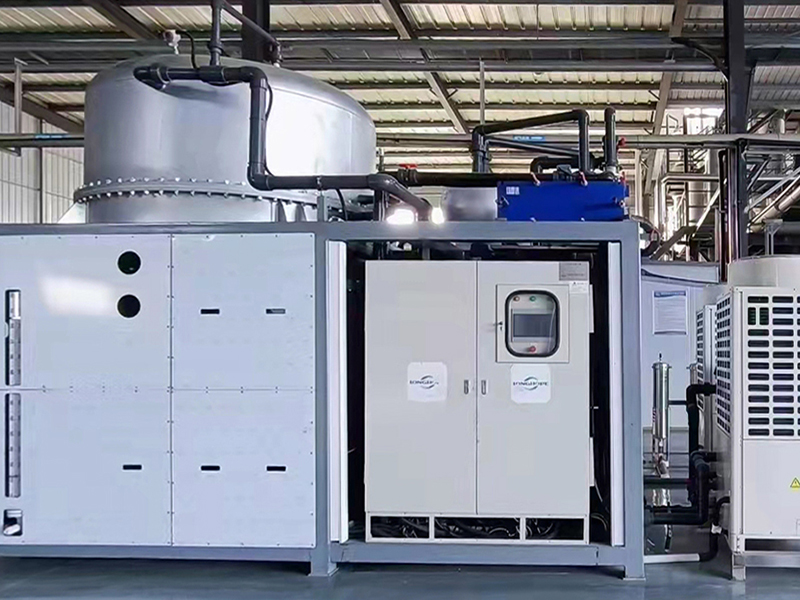

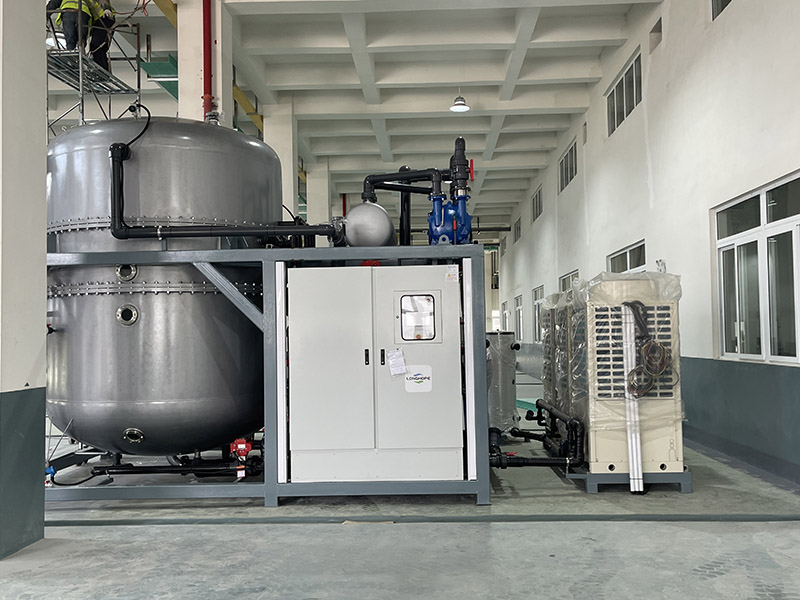
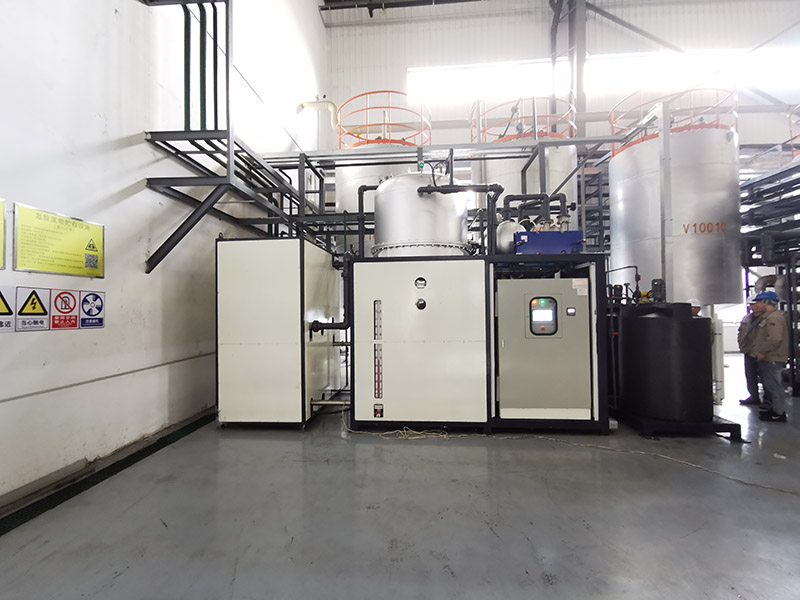
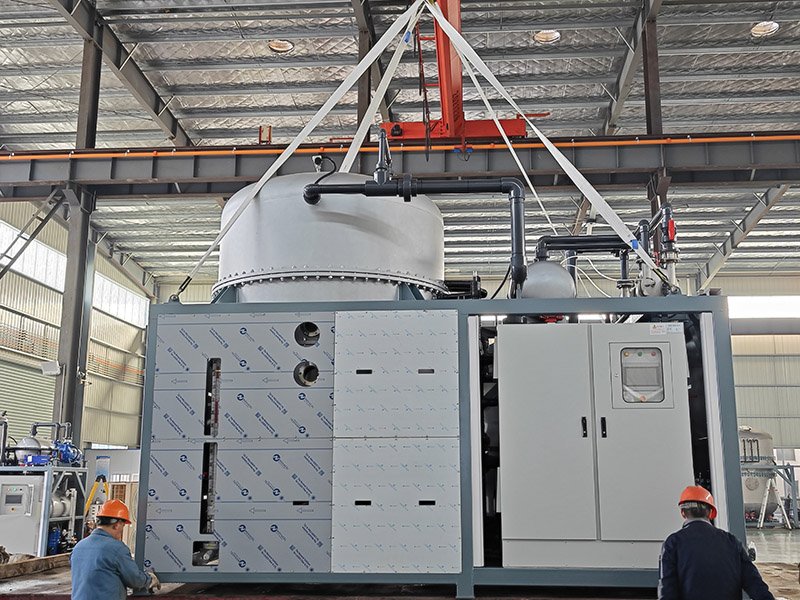
Low Temperature Evaporator V-HP-SF-2500 | 110 L/h | 18.13 kW | Trusted China Suppliers & Factory
Efficient & Advanced Evaporation Technology
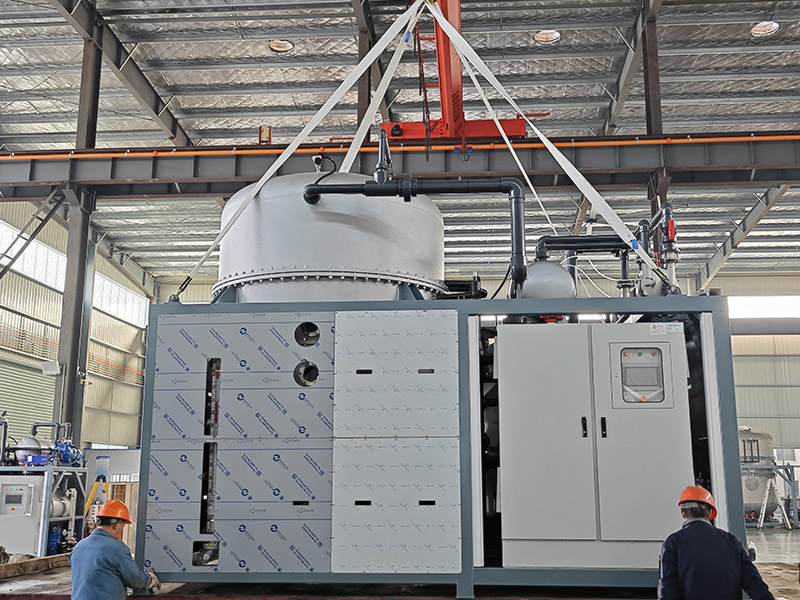
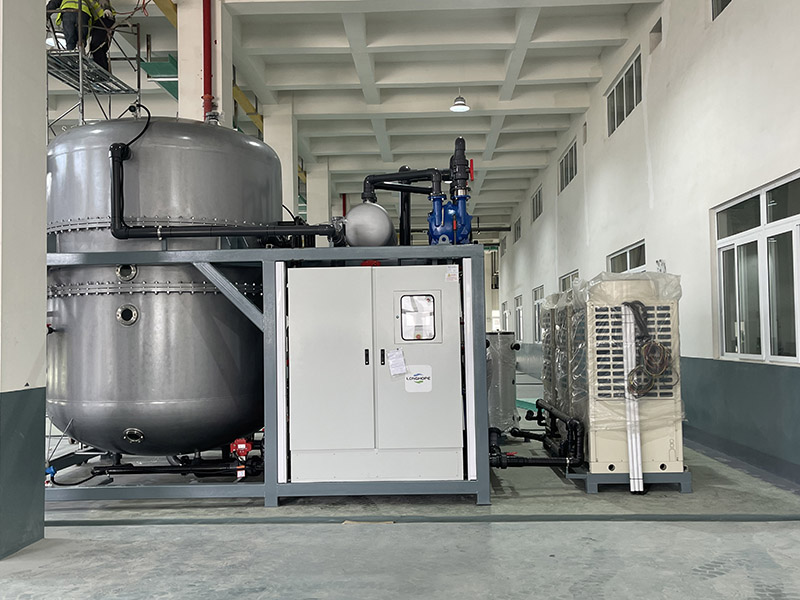
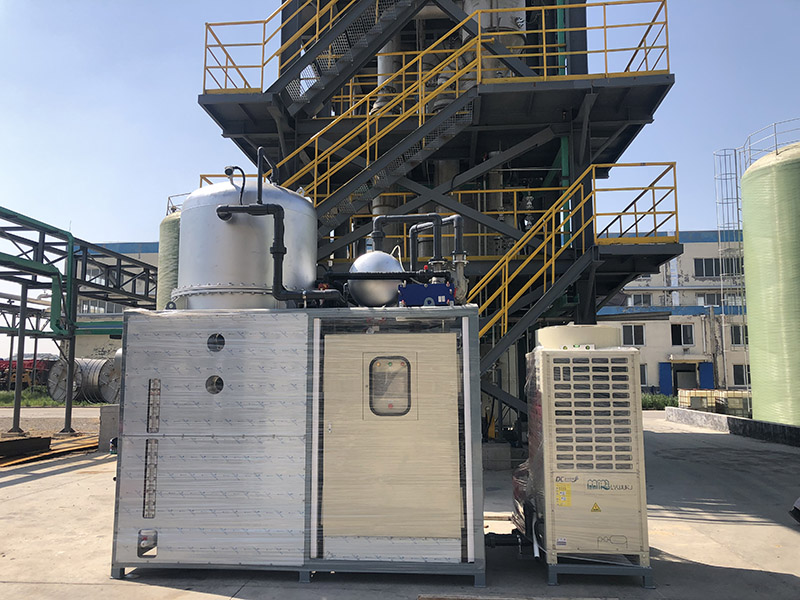
Heat pump low temperature evaporator is an efficient and advanced evaporation technology. Its main function is to reduce the boiling point of the stock solution under vacuum negative pressure environment, so that the stock solution boils and evaporates at a low temperature of about 35℃.
This process allows the evaporating steam to condense into liquid water, which is discharged through drains. Because of the difference in the specific gravity of the water, the concentration reduction effluent rate of the equipment can reach 95%, which greatly reduces the cost of waste liquid treatment for enterprises.
Integrated Control
Modular design, PLC automatic control, to achieve no manual duty.
Tube - Forced Circulation
Heat energy circulation transfer, less scaling. If other heating methods are used, there will be scaling, high energy consumption, and later affect the stability of the equipment.
Waste Liquid Evaporation Unit
Composed of vacuum system, evaporator, volatilization chamber and other parts, waste liquid in the vacuum negative pressure state to achieve efficient separation of water and stock liquid.
Intelligent Operation
Fully automatic operation, remote monitoring of mobile device terminals.
The heat pump evaporation technology, as an advanced and efficient evaporation method, is widely applied in the concentration, crystallization, and drying in many industries such as emulsified liquid wastewater, electroplating wastewater, RO concentrate, high-salinity wastewater, landfill leachate, printing and dyeing wastewater, spray paint wastewater, and pickling wastewater.
Modular Design & Wastewater Treatment Scope
Modular design, the use of electricity to vaporize wastewater at a low temperature of 35℃, water molecules and pollutants separation, obtain clear distilled water, can reduce COD up to 99%, for water reuse or standard discharge, automatic operation of the equipment without personnel duty.
Emulsified Liquid Wastewater
Electroplating Wastewater
RO Concentrate
High-Salinity Wastewater
Landfill Leachate
Printing & Dyeing Wastewater
Spray Paint Wastewater
Pickling Wastewater
Our Dedicated Team
We are a professional team, our members have many years of experience in international trade. We are a young team, full of inspiration and innovation. We are a dedicated team. We use qualified products to satisfy customers and win their trust. We are a team with dreams. Our common dream is to provide customers with the most reliable products and improve together. Trust us, win-win.
Frequently Asked Questions
Q1. What is the operating temperature of the heat pump low temperature evaporator?
The heat pump low temperature evaporator reduces the boiling point of the stock solution under a vacuum negative pressure environment, allowing it to boil and evaporate at a low temperature of about 35℃.
Q2. How much can the system reduce the cost of waste liquid treatment?
Due to the difference in the specific gravity of the water, the concentration reduction effluent rate of the equipment can reach up to 95%, which greatly reduces the overall cost of waste liquid treatment for enterprises.
Q3. What are the benefits of using a tube-forced circulation system?
The tube-forced circulation design ensures efficient heat energy circulation transfer and results in less scaling. Unlike other heating methods, it prevents high energy consumption and maintains long-term equipment stability.
Q4. What industries can apply this heat pump low temperature evaporation technology?
It is widely used for concentration, crystallization, and drying in industries dealing with emulsified liquid wastewater, electroplating wastewater, RO concentrate, high-salinity wastewater, landfill leachate, printing and dyeing wastewater, spray paint wastewater, and pickling wastewater.
Q5. How efficient is the COD reduction and water purification process?
By separating water molecules from pollutants at a low temperature of 35℃, the system obtains clear distilled water and can reduce COD by up to 99%, making the water suitable for reuse or standard discharge.
Q6. Does the equipment require manual supervision?
No, the equipment features modular design, PLC automatic control, and fully automatic operation with remote monitoring via mobile device terminals, achieving efficient operation without manual duty.